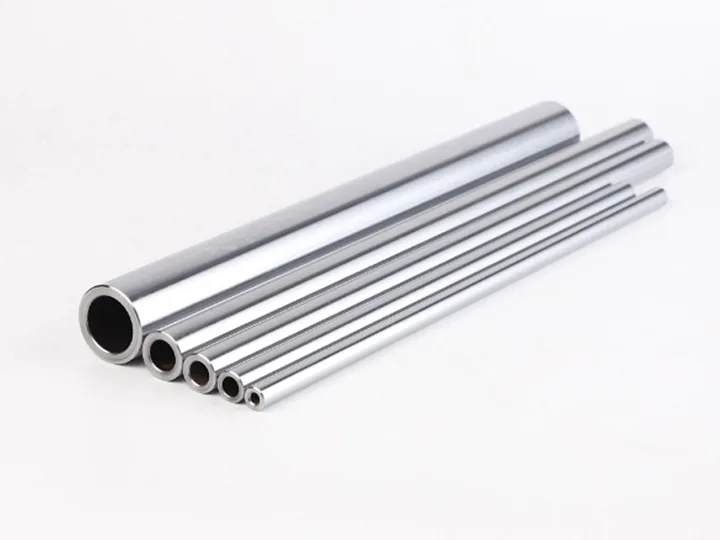
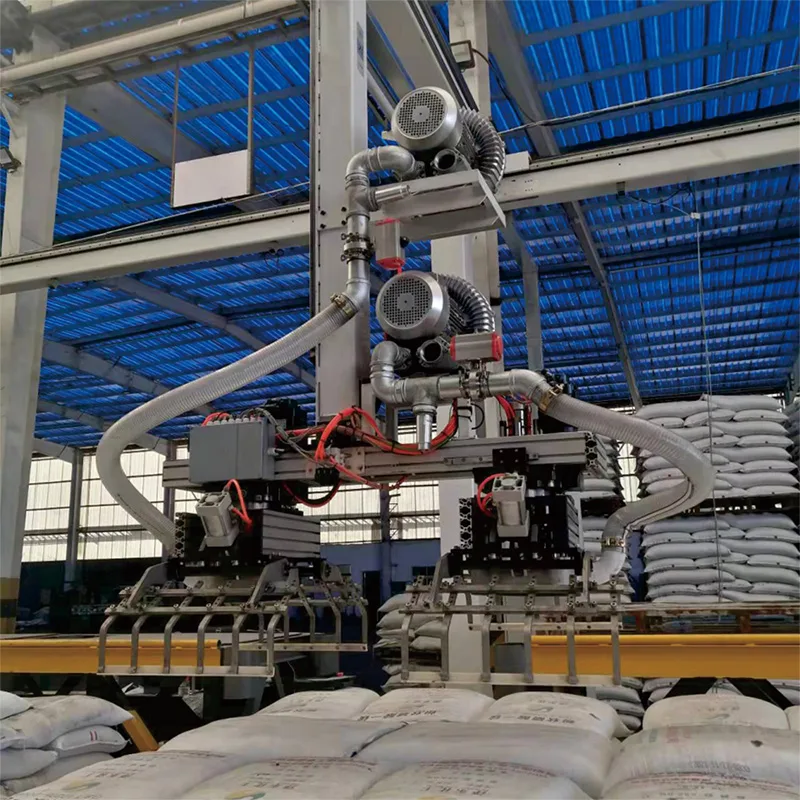
Stainless steel is the default material for packaging machinery because it combines corrosion resistance, cleanability, mechanical strength, and food-safety compliance — all of which are mandatory for hygienic processing. The specific grade is selected to match the product, the cleaning regime, and the regulatory environment.
The most common stainless grades for packaging machinery are 304 (18Cr-8Ni), 316 (16Cr-10Ni-2Mo), and 430 (16Cr, ferritic). Each grade has a specific role.
When Is 304 Stainless Steel the Correct Choice?
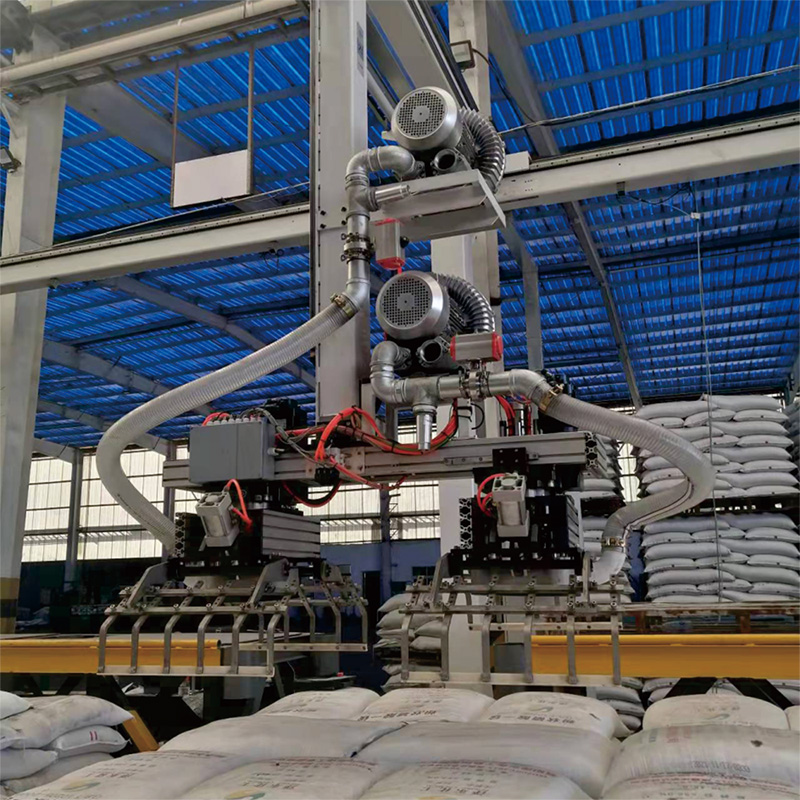
304 stainless steel is the correct choice for general-purpose packaging machinery components in non-corrosive product environments — conveyors, guards, frames, shafts, and standard fittings. It is the most widely used stainless grade.
Typical 304 applications:
Machine frames and support structures.
Conveyor shafts, rollers, and bearings.
Guards and safety covers.
Standard fittings (valves, pumps, tanks).
Architectural panels and access doors.
Product contact surfaces in dry-goods packaging.
304's corrosion resistance is adequate for most washdown chemicals, mild acids, and atmospheric exposure. It is not recommended for chloride-rich environments (e.g., salt, dairy, seafood) where 316 is preferred.
When Is 316 Stainless Steel Required?316 stainless steel is required for chloride-rich, acidic, or pharmaceutical environments — dairy, seafood, brewery, pharmaceutical, and outdoor coastal applications. The 2–3% molybdenum addition improves chloride pitting resistance.
316L (low-carbon variant) is preferred for welded pharmaceutical and food-contact equipment to avoid sensitization (chromium carbide precipitation at grain boundaries) that can compromise corrosion resistance.
When Is 430 Stainless Steel Acceptable?430 stainless steel is acceptable for indoor, low-corrosion packaging machinery components where cost is a primary driver and the surface finish does not need to be highly polished. 430 is ferritic, magnetic, and lower-cost than 304.
Typical 430 applications:
Indoor equipment panels and guards.
Decorative trim and nameplates.
Equipment enclosures (indoor, non-washdown).
Low-stress structural brackets.
430 is not suitable for chloride-rich environments, for outdoor exposure, or for food-contact surfaces. Its corrosion resistance is significantly lower than 304.
What Surface Finishes Are Available?Stainless steel surface finishes are specified by a standard designation (No. 2B, BA, No. 4, No. 8, electropolished) and by a Ra value for hygienic surfaces. Each finish has a specific application.
Hygienic surfaces (food contact, pharmaceutical) typically require Ra ≤ 0.8 μm and a smooth, crevice-free geometry. Electropolishing further reduces the Ra and removes surface imperfections that could harbor bacteria.
What Are the Fabrication Process Options?Stainless steel packaging machinery components are fabricated by CNC machining (for shafts, fittings, and complex 3D shapes), sheet metal forming (for enclosures, panels, and frames), or a combination of both. Each process has specific considerations for stainless.
Chuangling's CNC Turning, CNC Milling, and Sheet Metal capabilities cover the full fabrication range.
What Are the Welding Considerations?Stainless steel welding requires specific procedures to maintain corrosion resistance, avoid sensitization, and achieve the required surface finish. Standard welding procedures per AWS D1.6 or EN ISO 15614-1 cover the major grades.
Weld discoloration (heat tint) is a chromium-depleted zone that reduces corrosion resistance. Removal by pickling, passivation, or electropolishing restores the corrosion resistance and the hygienic surface.
What Are the Tolerance Requirements?Stainless steel packaging machinery components typically require ISO 2768-mK to -fine tolerances, with tighter requirements on mating surfaces, sealing surfaces, and rotating components. The tolerance allocation depends on the function.
Tight tolerances are concentrated on the rotating and sealing surfaces. General sheet metal tolerances are looser, but surface finish is held to hygienic-grade for food-contact surfaces.
How Is Surface Finish Verified?Surface finish is verified with a calibrated profilometer (contact or laser) at multiple locations on the surface, with the result compared to the specification. Verification is performed on first article, on a sampled basis during production, and on every part for critical features.
Chuangling's inspection equipment includes calibrated profilometers and the testing capability for the major surface-finish specifications.
What Are the Common Failure Modes?Stainless steel packaging components fail by corrosion (pitting, crevice, stress corrosion cracking), wear, fatigue, or contamination — each preventable by the right material, finish, and operating procedure.
Each failure mode is preventable by the right specification. The most common error is using 304 in a chloride environment, which leads to pitting within months.
How Are Export Projects Handled?Packaging machinery components exported to the EU, USA, or other markets must comply with the destination's food-contact regulations and material certifications. Common requirements:
Chuangling's export team prepares the declarations of compliance, the material certificates, and the surface-finish documentation per the destination's requirements.
Frequently Asked QuestionsQ: What is the difference between 304 and 316 stainless steel?
A: 304 is an 18% chromium, 8% nickel austenitic stainless steel (AISI 304). 316 adds 2–3% molybdenum to improve chloride pitting resistance. 316 is preferred for chloride-rich environments (dairy, seafood, pharmaceutical, coastal); 304 is sufficient for general applications.
Q: What is the difference between 304 and 304L?
A: 304L is the low-carbon variant (carbon content ≤ 0.03%) of 304. The lower carbon content reduces the risk of sensitization (chromium carbide precipitation) during welding, making 304L preferred for welded food-contact equipment.
Q: Can Chuangling produce components in 316L stainless steel?
A: Yes. Chuangling produces 316L components for pharmaceutical, dairy, and marine applications. Material certificates (mill certs) are provided with each shipment.
Q: What surface finish is required for food-contact surfaces?
A: Food-contact surfaces typically require Ra ≤ 0.8 μm and a smooth, crevice-free finish. No. 4 (brushed, 150–180 grit) is the standard food-contact finish; BA or electropolished is required for dairy, pharmaceutical, and high-hygiene applications.
Q: Can stainless steel components be welded?
A: Yes, with appropriate procedures. TIG (GTAW) is preferred for stainless; filler metal 308L for 304, 316L for 316. Post-weld pickling and passivation restore corrosion resistance.
Q: What is passivation?
A: Passivation is a chemical treatment (typically nitric acid or citric acid) that removes free iron from the stainless surface and promotes the formation of the chromium-oxide passive layer. Passivation is required after welding, machining, or any process that may have contaminated the surface.
Q: What is electropolishing?
A: Electropolishing is an electrochemical process that removes a thin layer of metal from the surface, smoothing the microscopic peaks and valleys. The result is a smoother, more corrosion-resistant surface that is easier to clean. Electropolishing is standard for pharmaceutical and semiconductor equipment.
Q: Can Chuangling produce hygienic tubing assemblies?
A: Yes. Chuangling produces hygienic tube assemblies in 304L and 316L with orbital welding, sanitary fittings (DIN, ISO, Tri-Clamp), and the required surface finish. The assemblies are leak-tested and passivated before shipment.
Q: What is the minimum order quantity for stainless steel packaging components?
A: For standard machined components, the minimum is typically 10–50 pieces. For custom sheet metal enclosures, the minimum is 5–20 pieces. For hygienic tubing assemblies, the minimum is set by the welding qualification cost, typically 10–50 pieces.
ConclusionPackaging machinery components require careful stainless steel grade selection, surface finish specification, and fabrication process control to deliver hygienic, corrosion-resistant equipment. Chuangling Machinery's Packaging Machinery capability, supported by Stainless Steel Parts, Sheet Metal, CNC Turning, and CNC Milling, covers the full range from machined fittings to welded hygienic assemblies. Pair the material and finish specification with the Production Equipment review and the Quality documentation for a complete procurement picture.