In industrial process development, a better result from one trial does not necessarily mean the process has improved. A drying cycle may finish earlier, a heating system may reach its target temperature faster, or a modified operating condition may produce material with lower residual moisture. The result looks promising, but it needs to be examined in the context of normal process variation.
Raw material properties, initial moisture content, ambient conditions, equipment behaviour and measurement methods can all influence experimental results. Unless these factors are considered, it is easy to attribute an improvement to a process modification when the difference may have occurred naturally.
For engineers and process development teams, the objective is to establish whether a change produces a repeatable, measurable benefit under comparable operating conditions. This requires a reliable baseline, controlled experiments, repeat trials and a clear understanding of measurement uncertainty.
Why One Successful Trial Is Not Enough
Industrial processes rarely produce identical results in every run. Even when the equipment settings remain unchanged, small differences in material composition, particle size, loading depth, initial temperature or moisture content can affect the outcome.
Consider a drying process that normally takes around 120 minutes. After an airflow adjustment, one batch reaches the required final moisture content in 108 minutes. The reduction is encouraging, but it does not establish that the adjustment caused the improvement.
The original process might already produce drying times between 110 and 125 minutes. If so, the new result could reflect normal variation rather than a genuine change in performance.
The same issue occurs in industrial heating and thermal processing. A faster heating cycle may result from a lower initial material temperature difference, a lighter load or improved contact between the material and the heat-transfer surface. Unless these factors are accounted for, the contribution of the modified operating condition remains uncertain.
A sound evaluation therefore asks three questions:
- Is the difference larger than the variation normally observed in the existing process?
- Can the improvement be reproduced under comparable conditions?
- Does the change deliver a practical benefit without compromising product quality or other operating requirements?
These questions provide a more reliable basis for process decisions than selecting the best result from a series of experiments.
1. Establish a Representative Baseline
Before testing a proposed improvement, engineers need to understand how the existing process performs under normal operating conditions.
A baseline is not simply the result of one reference batch. It should reflect the process's usual performance and the variation that occurs between runs. If the baseline is based on an unusually poor batch, almost any subsequent trial may appear favourable.
For an industrial drying process, baseline measurements might include:
- Initial and final moisture content.
- Drying time and material temperature.
- Inlet air temperature, humidity and airflow velocity.
- Material loading, bed depth and residence time.
- Energy consumption per unit of material processed.
- Product quality, moisture uniformity and material degradation.
The measurements should reflect the intended improvement. If the objective is to reduce drying time, the comparison must use a consistent final moisture specification. Otherwise, a shorter cycle may simply mean that the material has not been dried sufficiently.
Material characteristics also need to be documented. Differences in particle size, initial moisture content, bulk density and thermal sensitivity can change drying behaviour, even when the same equipment settings are used.
A representative baseline provides the reference needed to judge whether the modified process performs differently and whether that difference is operationally meaningful.
2. Repeat Trials to Check Reproducibility
Repeat trials help establish whether a favourable result reflects a consistent process response or an isolated occurrence.
The number of trials required depends on the variability of the process, the size of the expected improvement, the confidence needed for the decision and the consequences of getting it wrong. Three runs may be useful for preliminary screening, but they are not automatically sufficient to validate a process change.
Consider the following illustrative results for a drying-time comparison.
TrialExisting processModified process1120 min108 min2116 min111 min3124 min109 minAverage120 min109.3 minIllustrative data only; these are not actual experimental results from KRDC.
The modified process has an average drying time approximately 10.7 minutes lower than the existing process, representing a reduction of about 8.9%.
The repeated results provide more evidence than a single successful run. However, three trials alone cannot establish how the process will perform across different material batches, operating days or production scales. Additional testing may be needed, particularly if the baseline has substantial variability.
It is also important to distinguish repeatability from reproducibility. Repeatability concerns the consistency of results under similar conditions, using the same equipment and measurement procedure. Reproducibility examines whether the findings remain consistent when relevant conditions change, such as the material batch, operating day or equipment setup.
For industrial process development, both can matter. A modification that performs consistently during laboratory testing may still behave differently when material properties or production conditions vary.
3. Use Control Experiments to Identify the Cause
A control experiment helps separate the effect of a proposed change from other factors that could influence the outcome.
Suppose an engineer increases both the drying temperature and airflow velocity. The material dries faster, but the experiment does not reveal which adjustment produced the result. The two changes may have contributed independently, interacted with each other or had different effects on product quality.
A controlled comparison reduces this uncertainty by keeping relevant conditions consistent while evaluating the change of interest.
Depending on the process, this may involve:
- Comparing the established operating condition with the modified condition.
- Using comparable material samples with similar initial moisture content and particle size.
- Maintaining consistent material loading, sample preparation and measurement procedures.
- Checking instrument calibration and sensor placement before each test series.
- Randomising or alternating the order of trials to reduce the influence of time-related effects.
In drying studies, airflow and temperature deserve particular attention because their effects are not independent in every situation. Increasing airflow may improve convective heat transfer and remove humid air from the material surface. However, the benefit depends on the material, dryer design, air distribution and the resistance to internal moisture movement.
Similarly, increasing temperature may accelerate heat transfer and moisture evaporation, but it may also cause surface hardening, shrinkage or thermal damage in sensitive materials.
Where several operating variables may interact, a designed experiment can provide more useful information than changing one parameter at a time. Factorial designs, for example, can help identify individual parameter effects and interactions between temperature, airflow and other selected variables.
The objective is to determine not only whether the process changed, but also whether the evidence supports a causal link between the modification and the observed result.
4. Understand Measurement Uncertainty
An apparent improvement may be caused partly or entirely by limitations in the measurement method. This is particularly important when the observed difference is small.
Measurement uncertainty arises from several sources, including instrument calibration, sensor resolution, instrument drift, sample preparation, operator technique and the representativeness of the sample.
In an industrial drying trial, for example, a moisture analyser may report a lower final moisture content after a change in operating conditions. Before concluding that the modified process produces a drier product, the measurement method and its uncertainty should be reviewed.
Several factors require attention.
Instrument calibration and suitability
Temperature sensors, moisture analysers, flow meters and power meters should be appropriate for the measurement range and maintained according to the relevant procedures. An instrument that is poorly suited to the required precision may not reliably detect a small improvement.
Sampling method
A single moisture measurement may not represent an entire batch, especially when moisture distribution is uneven. Samples collected from different positions or depths may reveal variation that an average conceals.
Measurement repeatability
Repeated measurements of the same sample can help establish how much variation comes from the measurement procedure itself.
Resolution and detection limits
A reported numerical difference is not automatically a meaningful difference. If the change is comparable to the measurement system's limitations, the evidence may be insufficient to distinguish the two conditions reliably.
Combined uncertainty
When a performance indicator is calculated from several measurements, uncertainty in the individual measurements can affect the final result. For example, calculating energy consumption per kilogram of dried material involves both energy measurement and the determination of processed mass.
Measurement uncertainty should not be confused with process variability. Measurement uncertainty concerns the limits of determining a value, while process variability reflects real changes in the material or operating system. Both need to be considered when interpreting trial results.
5. Compare Variation, Not Just Average Performance
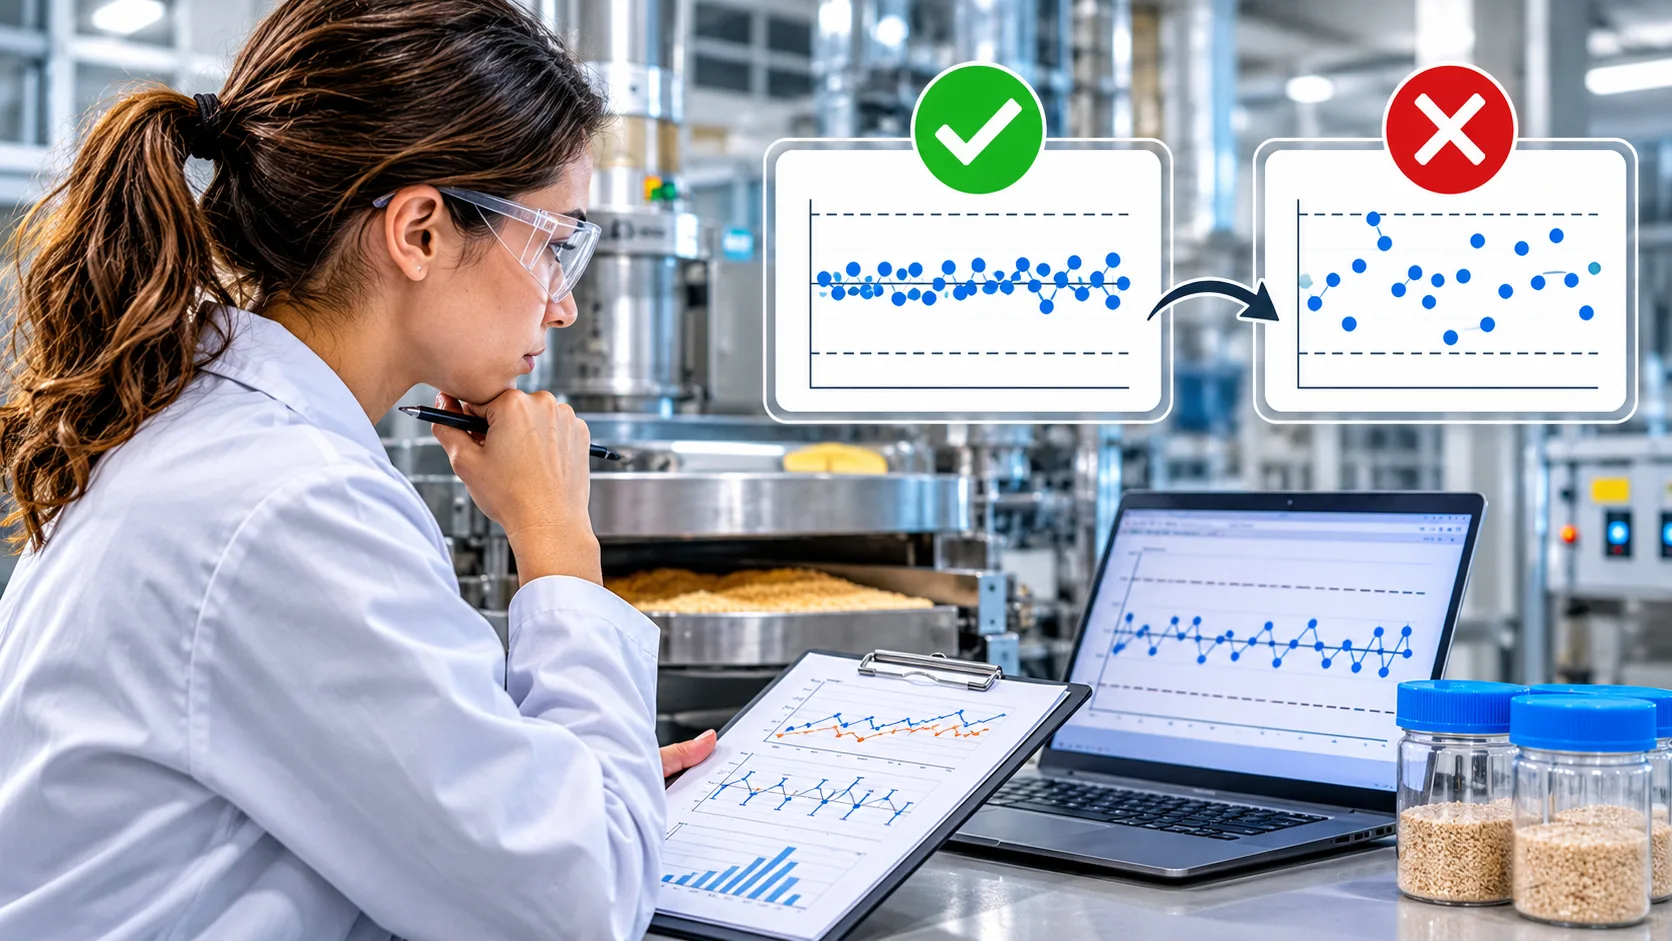
An average is useful for summarising results, but it does not show how consistently the process operates.
Two drying systems might achieve the same average drying time while exhibiting different levels of variation. One may produce relatively consistent cycles, whereas the other alternates between unusually fast and unusually slow runs.
The following statistical measures can help describe process performance:
- Mean: The average result across the observed trials.
- Standard deviation: A measure of how widely the results vary around the mean.
- Confidence interval: An estimate of uncertainty around a calculated quantity, such as the average difference between two process conditions.
- Control chart: A tool for assessing whether process behaviour remains statistically stable over time.
The appropriate analysis depends on the experimental design. When baseline and modified trials can be meaningfully matched, a paired analysis may be appropriate. For independent groups of trials, a method designed for independent samples may be more suitable.
Engineers should also distinguish statistical significance from practical significance. A statistically detectable improvement may be too small to justify a change in equipment settings, energy consumption or production procedures. Conversely, an improvement that could be valuable in production may require more data before its magnitude can be estimated with sufficient confidence.
Baseline variability is particularly important when many operating conditions are tested. If several trials are performed and only the most favourable result is selected, the apparent improvement may be exaggerated simply because the best result was chosen from a group of variable observations.
The stronger approach is to evaluate the complete set of relevant results against the established baseline and the predefined acceptance criteria.
6. Avoid Accepting Improvements Based on Selective Results
Testing multiple process settings increases the chance of observing an unusually favourable result, even when the underlying process has not improved.
For example, an engineer may test several combinations of temperature, airflow and residence time. If only the fastest run is reported, the selected result may reflect random variation rather than a reliable operating advantage.
This selection effect is one reason why experimental conclusions should be based on a documented test plan rather than the most attractive result.
Other common problems include:
- Selecting an unusually poor baseline run for comparison.
- Changing several parameters without recording their individual effects.
- Stopping testing as soon as a favourable result appears.
- Excluding unsuccessful trials from the final analysis.
- Focusing on one performance indicator while ignoring product quality or energy consumption.
These problems can be reduced by defining the evaluation criteria before the experiment begins.
For a drying process, the criteria might include cycle time, final moisture content, moisture uniformity and energy consumption. For a heating process, they could include heating time, temperature uniformity, product integrity and power demand.
The acceptance criteria should also identify the minimum improvement worth pursuing. This prevents small numerical differences from being treated as valuable simply because they favour the modified condition.
After the initial analysis, a confirmation trial or independent test series can help establish whether the selected operating condition delivers the expected benefit beyond the original experimental set.
7. Evaluate the Practical Value of the Improvement
A measurable change is not necessarily a useful improvement. The result must be evaluated against the requirements of the actual process.
Consider an increase in drying temperature. It may reduce cycle time, but it could also cause uneven moisture removal, surface hardening or damage to heat-sensitive components. Similarly, increasing airflow may improve moisture removal while increasing fan power consumption or causing particle entrainment.
These interactions make it important to evaluate the process as a whole rather than optimise a single variable in isolation.
Evaluation areaWhat to establishProcess performanceIs the improvement repeatable and large enough to matter?Product qualityAre moisture, composition, uniformity and other specifications maintained?Energy consumptionDoes the change reduce or increase total energy use per unit of acceptable product?Process stabilityDoes performance remain consistent between batches and operating periods?Equipment constraintsAre temperature, airflow, pressure and other operating limits respected?Scale-up potentialIs the improvement likely to persist at a larger processing capacity?Energy comparisons deserve particular care. A shorter cycle does not necessarily mean lower energy consumption. A system operating at a higher power level may complete the process faster but use the same or greater total energy. Energy per unit of acceptable product is often a more useful comparison than cycle time alone.
Scale-up introduces further considerations. Changes in material depth, equipment geometry, airflow distribution, heat-transfer area and residence time can alter the process response. A modification that performs well with a small sample may not produce the same result in a pilot unit or production-scale system.
Pilot testing and process validation can help identify these differences before a new operating condition is adopted routinely. The scope of testing should reflect the material, equipment, process complexity and potential consequences of failure.
8. Follow a Structured Process Validation Workflow
A consistent workflow helps engineers evaluate proposed improvements using comparable evidence.
Step 1: Define the objective
Specify the expected benefit, the primary performance measure and the conditions that must remain acceptable. A target such as reducing drying time should be accompanied by a clear final moisture requirement.
Step 2: Establish the baseline
Collect representative measurements under normal operating conditions. Record both average performance and the variation between trials, along with material properties and equipment settings.
Step 3: Plan the experiments
Identify the parameters to be changed, the variables to be controlled and the measurement methods to be used. Determine the number of trials based on expected variability, the desired confidence and the importance of the decision.
Step 4: Conduct and document repeat trials
Record all relevant results, including unsuccessful runs, deviations and unusual operating conditions. Documenting only favourable outcomes can distort the assessment.
Step 5: Analyse the evidence
Compare the modified process with the baseline using appropriate statistical methods. Consider measurement uncertainty, process variability, product quality and practical operating benefits.
Step 6: Confirm the findings
Where the initial results support an improvement, conduct additional testing under relevant conditions. Depending on the application, this may involve independent material batches, different operating days or pilot-scale trials.
The final conclusion should state what was demonstrated, under which conditions, and what remains uncertain. A change may be promising without yet being fully validated across the intended operating range.
The Role of Industrial Research and Development
Industrial research and development provide a structured way to investigate process behaviour, evaluate alternative operating conditions and establish the evidence needed for technical decisions.
In areas such as industrial heating, drying and thermal processing, this work may involve material characterisation, equipment parameter studies, pilot trials, troubleshooting and process performance evaluation. The purpose is to understand how the process responds to changes and determine whether the observed benefits can be reproduced under relevant conditions.
A research and development centre such as Kerone Research and Development Centre (KRDC) sits within this broader industrial R&D context. Process validation and experimental evaluation are relevant to the wider work of industrial research, although the specific tests, equipment and services available at any centre should be confirmed independently.
A useful experimental record should include the test objective, equipment configuration, operating parameters, material characteristics, measurement methods, individual trial results and deviations from the planned procedure. This information allows results to be reviewed and experiments to be repeated under comparable conditions.
The strength of an experimental conclusion depends on the quality of the evidence. If a process has been tested only with a limited sample size or within a narrow operating range, the findings should be reported accordingly rather than generalised to all materials or production conditions.
Conclusion
A true process improvement must be distinguished from the variation that occurs naturally in industrial experiments. One successful trial may identify a promising operating condition, but it does not establish repeatability, reliability or suitability for production.
A representative baseline, controlled comparisons, repeat trials and reliable measurement methods provide the foundation for a sound evaluation. Statistical analysis helps establish whether the observed difference is consistent with an actual change, while confirmation testing provides additional evidence under relevant operating conditions.
The final decision should consider more than the best recorded result. A worthwhile improvement is one that delivers a reproducible operational benefit while maintaining product quality, energy efficiency, process stability and the constraints of the intended application.